



Originating in the Bronze Age, heat treatment was further developed to process iron (blacksmithing) around 800 B.C., reaching a first peak with the production of Damascus steel in the beginning of the 10th century A.D. .
Iron was converted into steel by adding carbon, thus giving the alloy new properties like increased hardness. A large number of iron alloys and various elements have been investigated resulting in the development of new steel types suitable for many different applications. Another way to change the properties of steel is heat treatment, like annealing. As time plays a crucial role in this process, temperature-time diagrams have been developed. Today, many temperature-time diagrams have been evaluated to manufacture the best steel for a specific application. These diagrams show the correlation between time and heat and the respective structure (austenite, martensite, bainite) of the treated steel. Heat treatment is primarily performed in hardening shops. The materials treated in hardening plants are mostly the same and reproducible, reliable, and comparable results are mandatory. For effective process control a large number of samples has to be tested. Due to this high throughput, the sample preparation process should be simple and fast. Moreover, the preparation must result in excellent sample flatness to ensure easy and error-free surface inspection.
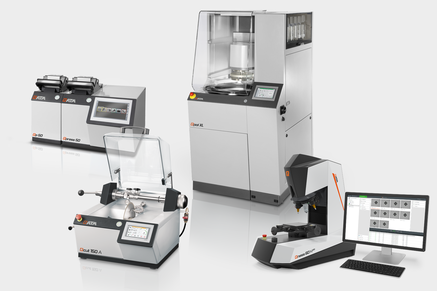
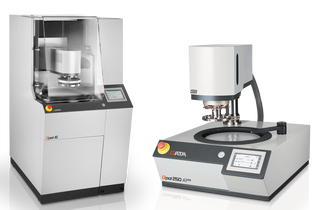
QATM предлагает решения для всех задач материаловедения
Materialographic Preparation Process
As a consequence of all these requirements, the preparation method should include:
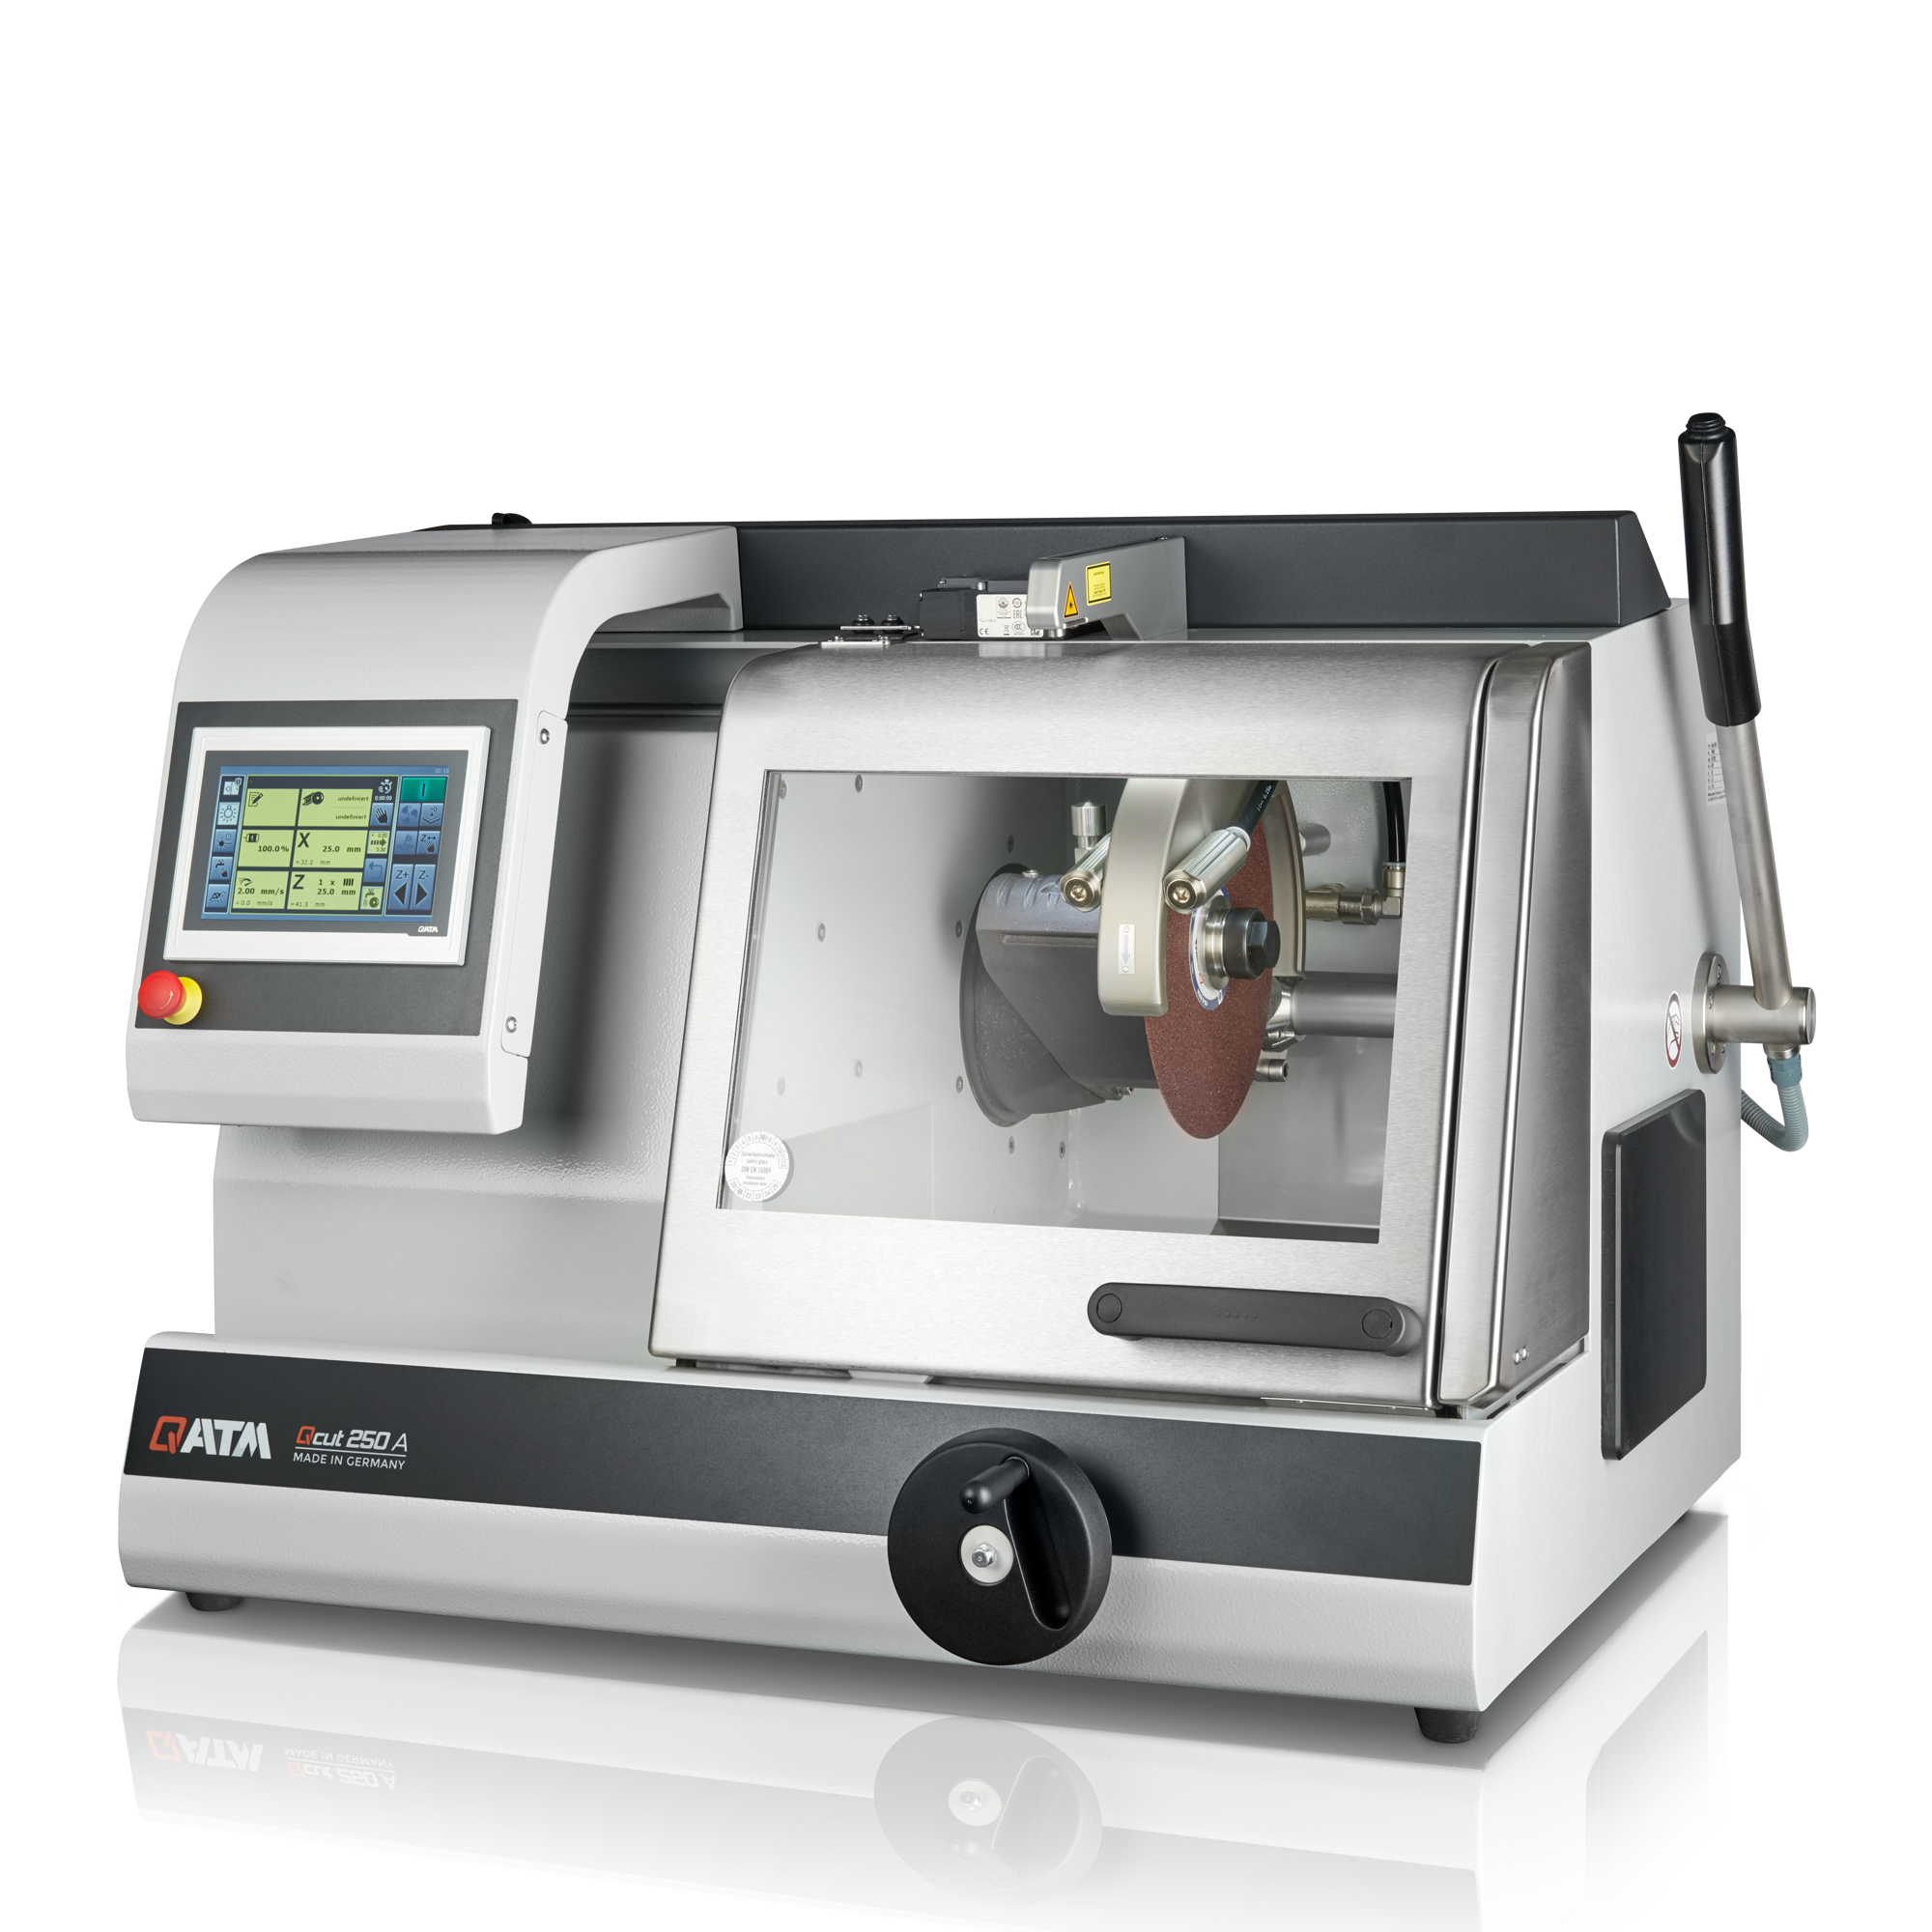
- fast and gentle sectioning of samples
- fast mounting yielding plane surface
- fast and gentle grinding/polishing
Методы пробоподготовки
Метод 1
This method has been well established for a long time. Due to the hardness of the heat-treated samples, the lifetime of the SiC Paper is quite short, resulting in relatively high costs for consumable consumption.
The preparation is as follows:
| Шаг | Medium | Смазка / суспензия | Скорость(оборотов в минуту ) | Скорость(оборотов в минуту ) | Держатель образца | Одиночное усилие(№ ) |
|---|---|---|---|---|---|---|
| Grinding | SiC, P180 | Вода | 300 | По часовой стрелке | 30 | До плоскости |
| Grinding | SiC, P320 | Вода | 300 | По часовой стрелке | 30 | 1:00 |
| Grinding | SiC, P600 | Вода | 300 | По часовой стрелке | 30 | 1:00 |
| Grinding | SiC, P1200 | Вода | 300 | По часовой стрелке | 30 | 1:00 |
| Полировка | IOTA | Dia complete, 3 | 150 | По часовой стрелке | 30 | 5:00 |
Метод 2
Planar grinding with a stone offers the advantage of a fast and cost-efficient preparation. But this involves an investment for a special machine. Nevertheless, the overall preparation time is reduced as no SiC papers need to be changed. Additionally, diamond lapping discs can be used, which have a long lifetime.
| Шаг | Medium | Смазка / суспензия | Скорость(оборотов в минуту ) | Скорость(оборотов в минуту ) | Держатель образца | Одиночное усилие(№ ) |
|---|---|---|---|---|---|---|
| Grinding | Камень, P100 | Вода | fixed | По часовой стрелке | 30 | До плоскости |
| Предварительная полировка | Galaxy Contero | Dia complete, 9 мкм | 150 | По часовой стрелке | 30 | 4:00 |
| Полировка | IOTA | Dia complete, 3 мкм | 150 | По часовой стрелке | 30 | 4:00 |
To avoid the investment for a new machine, diamond grinding discs for planar grinding may be utilized offering the advantage of using standard grinding and polishing equipment.
Метод 3
The Galaxy grinding disc is very stiff and yields plane surfaces even if the hardness of the sample surface varies.
| Шаг | Medium | Смазка / суспензия | Скорость(оборотов в минуту ) | Скорость(оборотов в минуту ) | Держатель образца | Одиночное усилие(№ ) |
|---|---|---|---|---|---|---|
| Grinding | Galaxy red | Вода | 300 | По часовой стрелке | 30 | До плоскости |
| Предварительная полировка | Galaxy Contero | Dia complete, 9 мкм | 150 | По часовой стрелке | 30 | 5:00 |
| Полировка | IOTA | Dia complete, 3 мкм | 150 | По часовой стрелке | 30 | 4:00 |
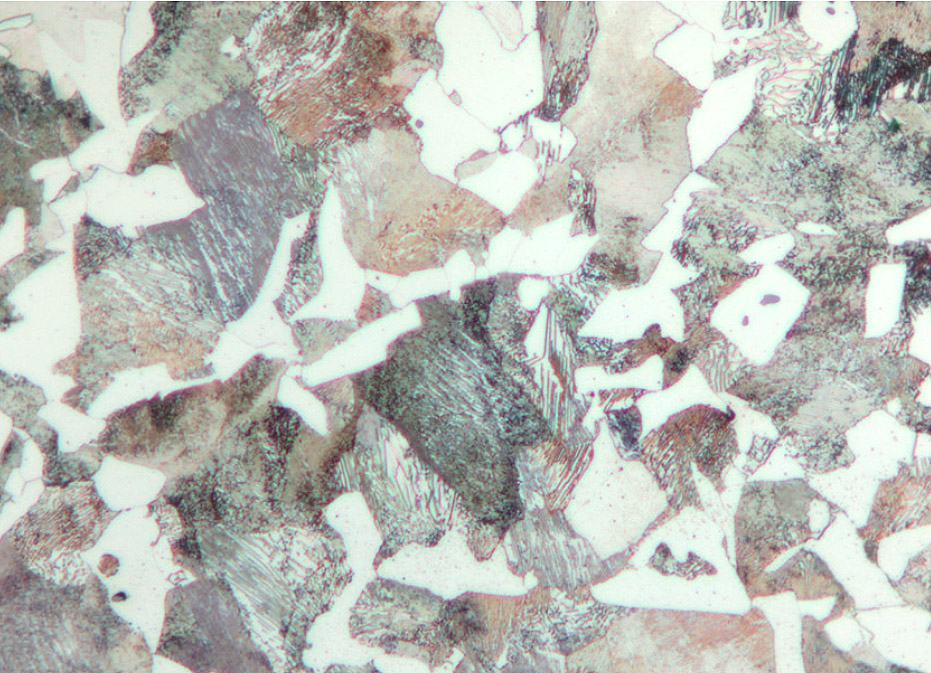
Ferrite-Pearlite, etched with 3% Nital, brightfield 20x
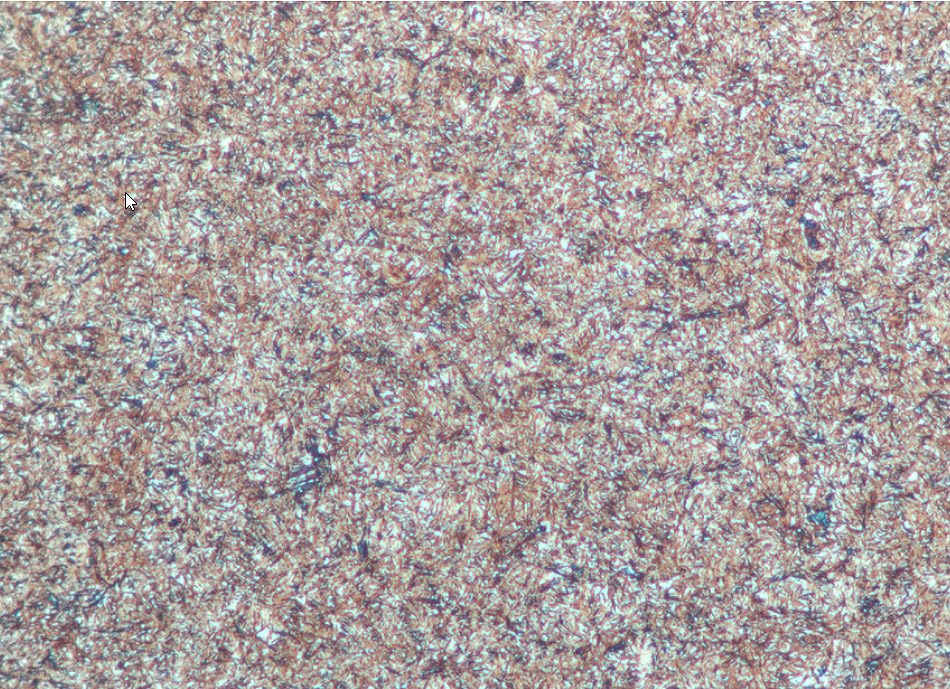
Martensitic structure after heat treatment, etched with 3% Nital, brightfield 20x
Заключение
В закалочных цехах требования к подготовке образцов включают короткое время подготовки, высокую производительность, надежные результаты с хорошей плоскостностью образцов для испытаний на твердость или исследований поверхности. Метод подготовки с использованием шлифовальной бумаги из карбида кремния SiC требует относительно больших затрат, а использование шлифовального камня требует вложений в специальный станок. Метод использования притирочных дисков дает преимущество использования существующих машин и длительного срока службы расходных материалов, обеспечивая наилучшую экономическую эффективность и удовлетворяя всем необходимым требованиям подготовки.
Contact us today
QATM offers a wide range of innovative machines for metallographic mounting, from robust hot mounting presses to devices for cold mounting under UV irradiation. Accompanying QATM mounting consumables are thoroughly tested and selected for perfect interaction with our machines. Contact us for a consultation, quote or to talk to one of our dedicated application specialists!